A global powerhouse in precision kitchenware manufacturing, exporting certified culinary hardware and modular storage systems to international trade partners across 65+ nations.
NORVEXA was founded to bridge the divide between high-end international culinary standards and factory-direct volume supply. Headquartered at our expansive manufacturing and logistics hub, we operate integrated tool-and-die fabrication, high-tonnage hydraulic deep-draw presses, progressive stamping lines, and automated cleanroom injection molding.
We cater directly to overseas supermarket retailers, hotel banquet suppliers, kitchenware brand licensors, and institutional catering distributors who demand certified material purity, on-time container dispatches, and responsive OEM engineering support.
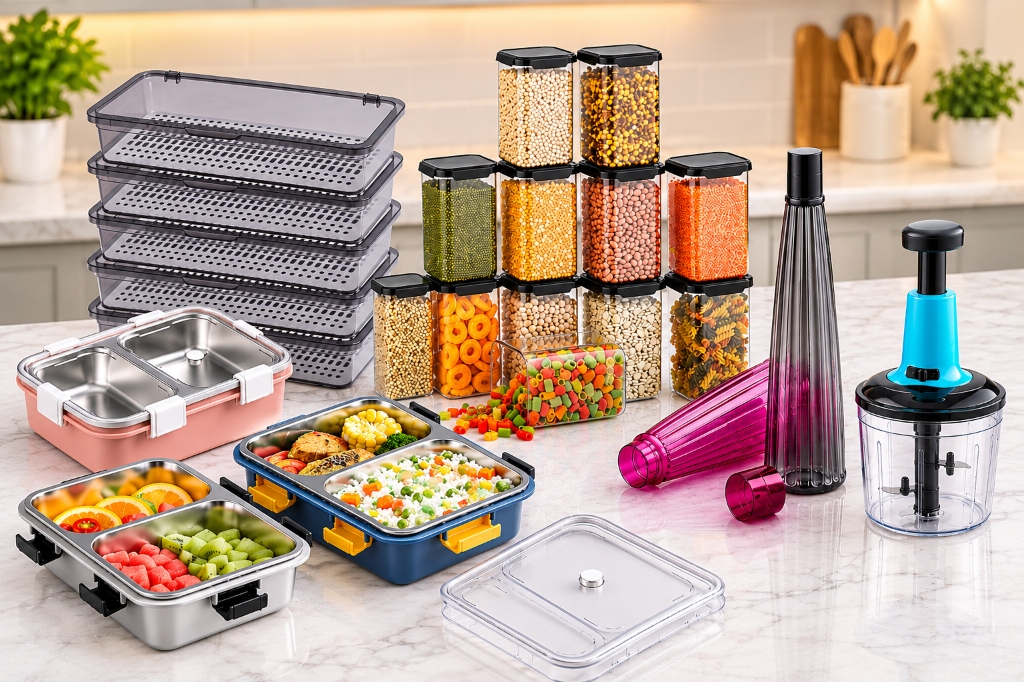
To engineer and deliver the highest grade of food-safe culinary hardware, stainless steel cookware, and modular food storage products that elevate culinary efficiency worldwide, while providing foreign importers with uncompromised transparency, competitive factory-gate pricing, and end-to-end maritime logistical execution.
To be the most reliable and technologically advanced kitchenware manufacturing partner across North America, Europe, the Middle East, and Oceania—recognized globally for material authenticity, ergonomic design innovation, and eco-conscious manufacturing practices.
The foundational pillars that guide our manufacturing benchmarks, global partnerships, and ethical commitments.
Every product engineered at NORVEXA adheres to strict global food-contact regulations, backed by transparent audit reports and reliable supply commitments.
Every NORVEXA product undergoes seven distinct quality inspections before export container loading.
Every stainless steel batch undergoes X-ray spectrometry to certify 18/8 (SS 304) chromium and nickel ratios before entering our stamping presses.
Food contact polymers, Tritan canisters, and silicone gaskets are certified non-toxic, BPA-free, and tested against acidic food migration.
Tested through 500+ commercial dishwashing cycles and extreme temperature shifts (-40°C to 230°C) without seal degradation or warping.
All airtight food containers and beverage flasks undergo pressurized air and immersion testing to verify 100% leak-proof hermetic lock seals.
Master cartons and retail presentation boxes pass international 10-point drop tests, guaranteeing zero freight damage during maritime sea voyages.
Independent QA inspectors verify barcode labels, pallet stacking patterns, moisture absorbents, and container seals prior to dispatch.
With proximity to primary deep-water sea container terminals, NORVEXA executes full container load (FCL) and consolidated less-than-container (LCL) shipments on weekly sailing schedules. Our multilingual export documentation department prepares complete compliance dossiers—including Certificates of Origin, legalized consular invoices, bill of lading (B/L), phytosanitary paperwork, and test reports conforming to destination customs regulations.